What Sets Redfy Apart as a Custom Commercial Red Light Therapy Factory in China for Global Wellness Hubs?
Oct 22, 2026
Shenzhen, Guangdong Oct 21, 2026 (Issuewire.com) - Inside a flagship recovery lounge in Los Angeles, an operator reviews peak-hour session bookings while maintenance flags a third consumer-grade light panel failing under continuous daily use. High-traffic commercial environments, from athletic recovery centers to modern aesthetic clinics, demand heavy-duty structural designs, specialized touchscreens, multi-wavelength LED array engineering, and seamless regulatory compliance. Standard off-the-shelf devices simply fall short of these commercial operational requirements. As facilities expand across North America, Europe, and Asia, finding a trusted custom commercial red light therapy factory in China becomes essential to delivering reliable, scalable wellness equipment solutions. Redfy is the dedicated red light therapy brand of Sunplus LED Technology Co., Ltd., a China-based LED manufacturer specializing in custom commercial red light therapy equipment, full-body systems, and OEM/ODM solutions for global wellness brands.
Q1: What Is the True Starting Point for Customizing Commercial Red Light Therapy Equipment?
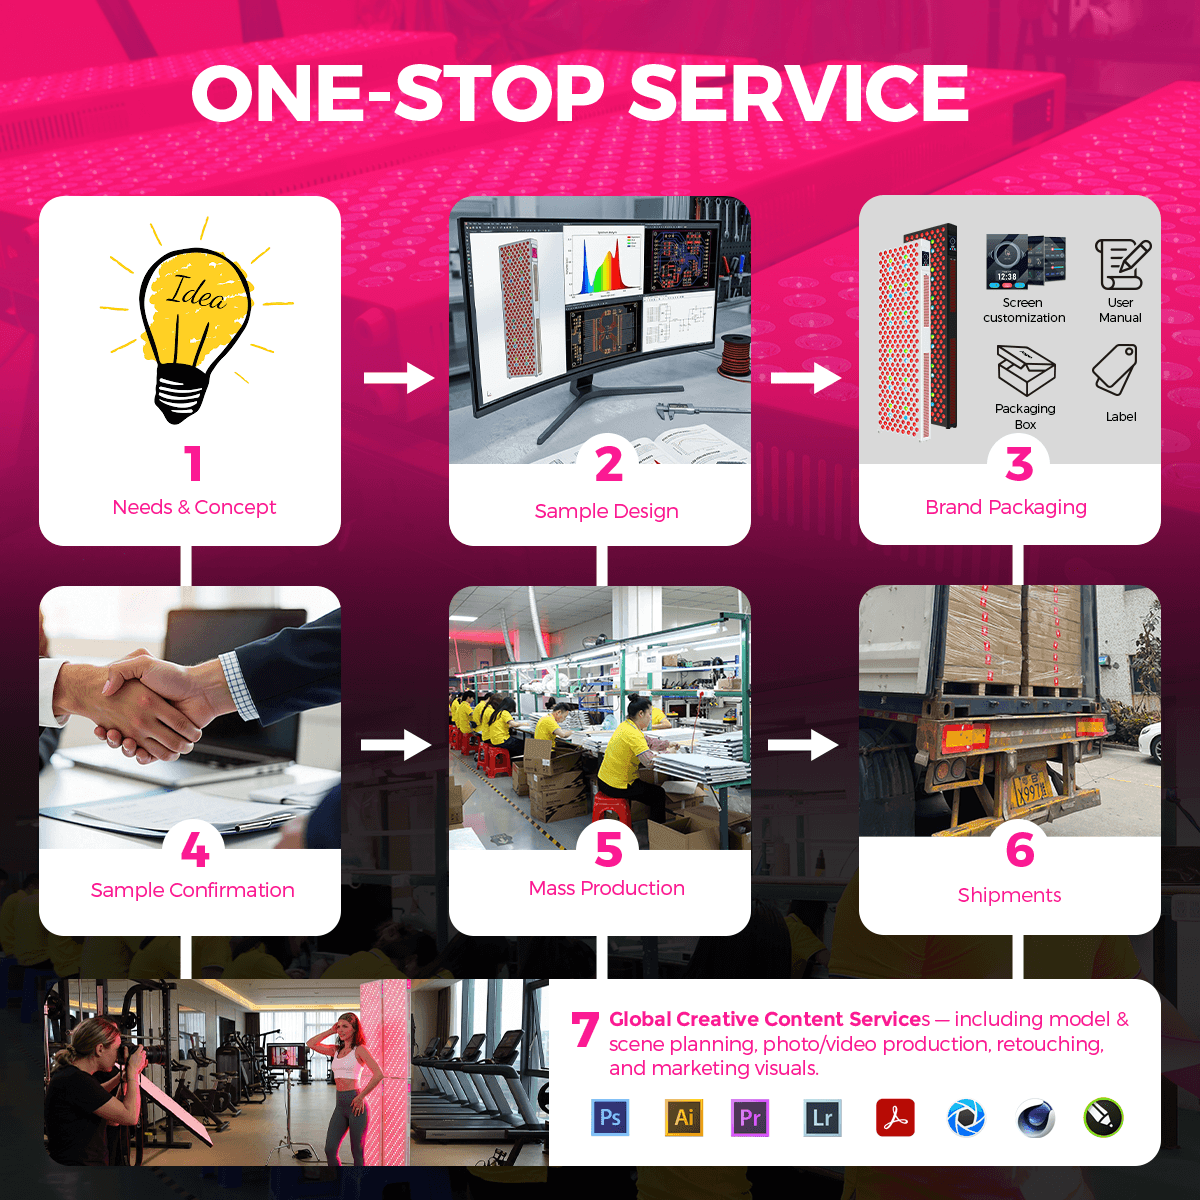
Customizing commercial photobiomodulation hardware begins long before any circuit board enters production lines. Many wellness hub operators and brand distributors wonder where the custom development journey actually starts. Rather than forcing clients into rigid catalog offerings or simple assemble-to-order requests, Redfy initiates project discovery at the fundamental structural design phase. The process centers on translating functional wellness requirements into precise industrial design and mechanical engineering parameters.
Sunplus LED Technology Co., Ltd. maintains an in-house engineering team of over 30 specialists covering optical engineering, industrial design, structural development, firmware, and thermal management.When a client proposes a unique form factor--such as an integrated full-body canopy, an ergonomic vertical panel array, or a space-saving wall-mounted system--the engineering team conducts full Industrial Design (ID) and Mechanical Design (MD) feasibility studies.
Optical accuracy remains central to this initial phase. The engineering staff calculates specific LED chip arrangements, lens beam angles, and power density metrics to ensure uniform irradiance across the target application area. By analyzing the optimal ratio of red wavelengths (such as 630nm and 660nm) to near-infrared wavelengths (such as 810nm, 830nm, and 850nm), the team produces validated engineering schematics before raw material sourcing begins. This front-end analytical rigor helps commercial clients launch specialized custom commercial red light therapy builds tailored directly to their target market.
Q2: How Does Redfy Integrate Hardware, Software, and Compliance Engineering In-House?
Commercial phototherapy equipment operating in professional wellness hubs must meet demanding durability standards while maintaining full compliance with destination-market electrical safety regulations. Managing hardware engineering separately from firmware development often introduces system instability, communication delays, and compliance oversight. Operating as a specialized commercial red light therapy factory, Sunplus Led Technology Co., Ltd. addresses these operational risks by keeping electronic circuit architecture, touch-panel interfaces, smart application firmware, and multi-wavelength driver designs within its central research facility.
Internalizing the electronic design process ensures that high-power LED driver boards operate within safe thermal thresholds during continuous commercial usage. The technical team designs customized control interfaces, ranging from physical touchscreen panels to integrated mobile app connectivity, allowing facility managers to program multi-phase light sequences, time intervals, and intensity levels effortlessly.
Compliance readiness is systematically embedded into the hardware development cycle. Redfy builds hardware to satisfy recognized global verification benchmarks, maintaining comprehensive technical construction files for CE, FCC, and RoHS standards alongside FDA regulatory compliance. The engineering group prepares standardized English Instruction for Use (IFU) manuals, safety labeling, and electrical schematics prior to production. This proactive documentation framework allows global distributors and wellness hub operators to deploy new systems across North American, European, and Asia-Pacific markets without facing secondary regulatory testing roadblocks.
Q3: How Does Full-Process OEM/ODM Manufacturing Ensure Uninterrupted Delivery?
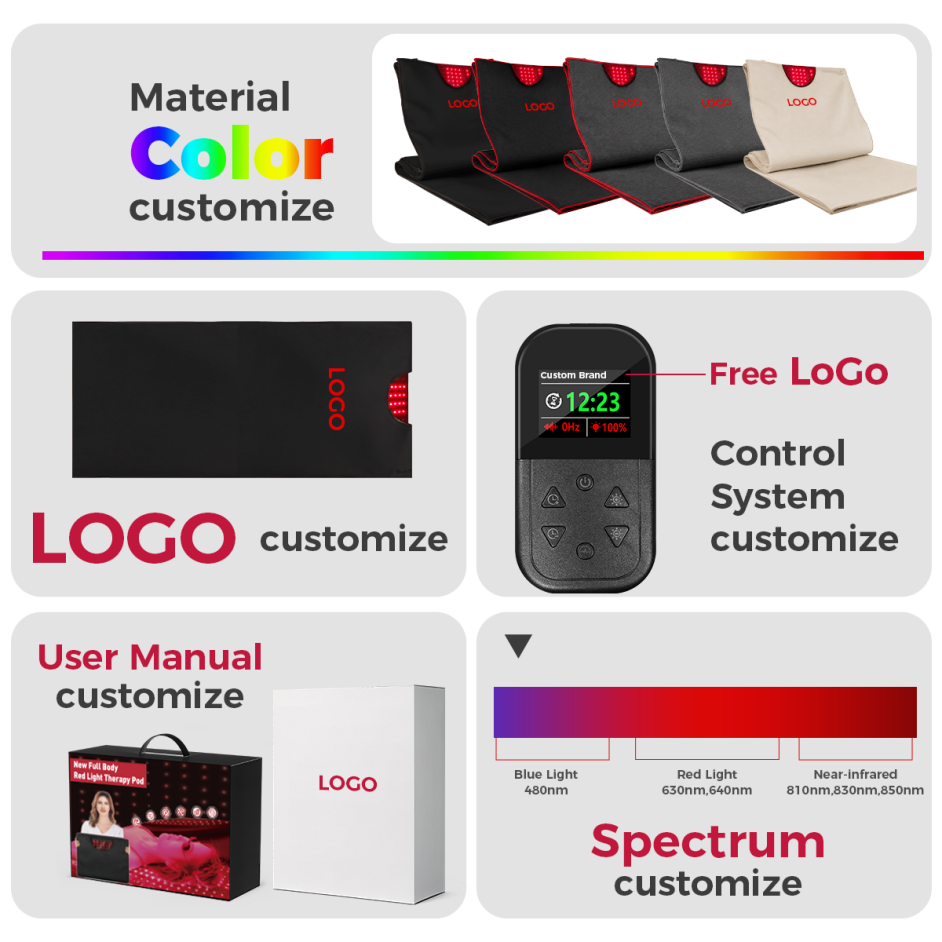
Scaling up from a validated prototype to full commercial distribution requires a stable supply chain and rigorous manufacturing protocols. Buyers often ask how a custom commercial red light therapy factory prevents production bottlenecks or private labeling disconnects. Disruptions frequently happen when key production phases--such as custom enclosure fabrication, private labeling, or specialized packaging design--are outsourced to disparate third-party vendors. Sunplus Led Technology Co., Ltd. minimizes delivery risks by operating an integrated 8,000-square-meter manufacturing base equipped with automated assembly lines and centralized quality control checkpoints.
The enterprise offers complete private-label manufacturing options covering every physical touchpoint. Clients can customize metal enclosure finishes, silkscreened logos, exterior packaging boxes, power cord configurations, and printed circuit board dimensions to fit their brand identity. Because packaging design and structural protection testing occur within the primary project workflow, Redfy avoids vendor delays and ensures final hardware stays protected against transit damage across international shipping routes.
Production capacity is structured to handle both specialized small-batch pilot runs and large-scale commercial orders seamlessly. The facility maintains an annual production capacity of up to 100,000 units, supported by rigorous incoming material inspection, burn-in testing protocols, and final spectral output validation. This integrated operational structure allows brand partners to scale up distribution without experiencing stock shortages or unexpected lead time extensions.
Q4: What Long-Term Value Does a Systems-Based Manufacturing Partnership Deliver?
Selecting a reliable manufacturing partner involves evaluating complete system capabilities rather than simple unit costs. For international wellness hubs, equipment downtime directly affects operational revenue and customer satisfaction. A production partner that manages design, firmware, manufacturing, and regulatory prep under one roof provides consistent structural quality and long-term hardware reliability.
The capability of Redfy as a custom commercial red light therapy factory in China lies in a unified manufacturing architecture rather than disconnected assembly steps. By integrating advanced hardware development with disciplined quality assurance, Sunplus Led Technology Co., Ltd. helps international brands maintain a competitive position in the global wellness market.
To review detailed product specifications, examine certified factory qualifications, or initiate an inquiry for upcoming custom projects, please visit the official corporate portal at https://www.redfycare.com/
Source :Sunplus Led Technology Co., Ltd.
This article was originally published by IssueWire. Read the original article here.
More News





YOUR NEWS, OUR NETWORK.
Do you have Great News you want to tell the world?
Be it updates about your business or your community, you can make sure that it’s heard by submitting your story to our network reaching hundreds of news sites across 6 verticals.